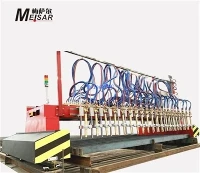
Industrial CNC Profile Plasma Cutting Machine
Heavy-Duty Gantry System for Precision Plate Profiling and Bevel Cutting
Product Evaluation & Technical Overview
The CNC Profile Plasma Cutting Machine is engineered for structural steel fabricators and heavy equipment manufacturers requiring high-precision contouring, accurate hole-to-edge ratios, and reliable multi-shift operation. Built around a stress-relieved steel gantry and dual-side AC servo drives, this platform delivers stable acceleration and consistent kerf quality across carbon steel, stainless steel, and aluminum plates.
Technical Specifications & Configuration
|
Technical Parameter |
Specification Range / Standard |
|
Effective Cutting Width |
2,000 mm - 4,000 mm (Customizable) |
|
Effective Cutting Length |
4,000 mm - 18,000 mm+ |
|
Plasma Source Options |
High-Definition HyPerformance (130A to 400A) / Air Plasma |
|
Max Piercing Capacity (Carbon Steel) |
Up to 32 mm (Production); up to 50 mm (Edge start) |
|
Max Bevel Cutting Angle |
+/- 45 deg (V, X, Y, K bevel configurations) |
|
Positioning Accuracy |
+/- 0.1 mm / m |
|
Repeatability |
+/- 0.05 mm |
|
Max Traverse Speed |
20,000 mm/min |
|
Drive System |
Dual AC Servo Motors & Drivers (Panasonic / Yaskawa) |
|
Height Control Response |
<= 1 ms real-time arc voltage feedback |
Application & Material Compatibility
This machine processes various industrial metal grades used in structural engineering and pressure vessel fabrication:
Carbon Steel (Q235, A36, S355):
Optimized for square edges and minimal dross, reducing secondary grinding time prior to welding.
Stainless Steel (304, 316L):
Utilizes oxygen-free or specialized gas mixing to prevent oxidation and maintain corrosion resistance along the cut edge.
Aluminum Alloys (5052, 6061):
High-speed plasma parameters control thermal distortion on plates ranging from 3 mm to 25 mm.
Typical Output Components:
Base plates, gussets, crane booms, ship ribs, wind tower flanges, and heavy weldment profiles.
Core Engineering & Manufacturing Process
Gantry Stress Relief: The heavy-wall box-welded gantry undergoes thermal annealing (furnace stress relief) followed by precision CNC gantry milling to eliminate residual structural stress and prevent thermal warping.
Rail Machining: Longitudinal rails are precision-machined on a 20-meter gantry milling machine, guaranteeing straightness tolerance under +/- 0.05 mm over the entire track length.
Drive Synchronization: Dual-side rack-and-pinion transmission utilizes helical gears with preload gearboxes to eliminate backlash during rapid directional changes.
Exhaust System: Segmented down-draft extraction tables with pneumatic zone dampers capture fumes directly beneath the active cutting area, complying with OSHA and EPA air quality standards.
Supplier Verification & Quality Control
Electrical Compliance:
Control cabinets wired to NFPA 79 / CE standards, utilizing industrial-grade enclosed terminal blocks, Schneider contactors, and shielded signal cables to withstand high-frequency plasma interference.
Component Documentation:
Full bill of materials provided with original manufacturer part numbers for all pneumatic, electronic, and motion control components.
Purchasing Decision & RFQ Guide
To configure a CNC profile plasma cutting machine that matches your production throughput, evaluate the following parameters before requesting a formal quotation:
Material Mix & Max Thickness: Specify the predominant thickness and grade (e.g., 20 mm A36 structural steel vs. 10 mm 304 stainless steel) to determine plasma power source amperage (130A, 260A, or 400A).
Table Dimensions: Match the effective cutting envelope to standard steel plate sizes used in your region (e.g., 2,000 x 6,000 mm or 8' x 24').
Extraction Requirements: Define whether your facility requires a dry dust collector or a water table based on local environmental regulations.
Software Ecosystem: Confirm compatibility with your existing CAD/CAM nesting software (e.g., SigmaNEST, ProNest) or evaluate the included industrial CNC controller package.
Frequently Asked Questions
Q: What is the edge angularity tolerance on 20 mm carbon steel when using high-definition plasma?
A: With a properly tuned high-definition plasma system and fresh consumables, edge angularity on 20 mm mild steel falls within ISO 9013 Range 3 to Range 4 (typically between 2 deg and 4 deg), depending on cutting speed and amperage.
Q: How does the Torch Height Control (THC) prevent torch collisions during plate warping?
A: The capacitive THC uses real-time arc voltage sampling combined with an ohmic initial height sense (IHS). If the torch encounters a tipped plate edge or slag buildup, an integrated magnetic breakaway switch immediately triggers an emergency stop to protect the torch body and consumables.
Q: What utility requirements are needed on the shop floor prior to installation?
A: Power Supply: 3-phase 380V/480V, 50/60Hz (amperage dependent on plasma source size).
Compressed Air: Clean, dry, oil-free air supply at 0.8 MPa (8 bar) with a minimum flow rate of 0.5 m^3/min for plasma gas and pneumatic valves.
Assist Gases: Industrial grade Oxygen, Nitrogen, Argon-Hydrogen mix (depending on cutting configuration).
Q: Are replacement consumables and spare parts proprietary?
A: No. The cutting torches and consumable stacks utilize standard industrial geometries compatible with major global torch standards, allowing your procurement team to source consumables locally without vendor lock-in.
Companion Tools for Sales & Engineering Conversion
Internal RFQ Data Intake Checklist (For Sales & Engineering)
When an inquiry arrives, use this checklist internally to ensure all critical variables are gathered before issuing a formal quotation:
Plate Material Grades: (E.g., A36 carbon steel, 304 stainless steel, 5052 aluminum)
Maximum & Nominal Thickness: (E.g., piercing up to 32 mm, continuous cutting at 12 mm)
Working Envelope (Bed Size): (E.g., 2,000 x 6,000 mm or custom dimensions)
Plasma Source Requirements: (E.g., High-Definition 130A / 260A / 400A or standard air plasma)
Bevel Cutting Requirements: (E.g., Standard square edge only vs. +/- 45 deg V/X/Y/K bevel capability)
Exhaust / Dust Collection: (E.g., Dry dust collector with pneumatic dampers vs. local water table provision)
Facility Utilities Available: (E.g., 3-phase 480V / 60Hz or 380V / 50Hz; compressed air supply specs)
CAD/CAM Software Integration: (E.g., Existing SigmaNEST / ProNest seat compatibility)
Hot Tags: cnc profile plasma cutting machine, China cnc profile plasma cutting machine manufacturers, suppliers, factory