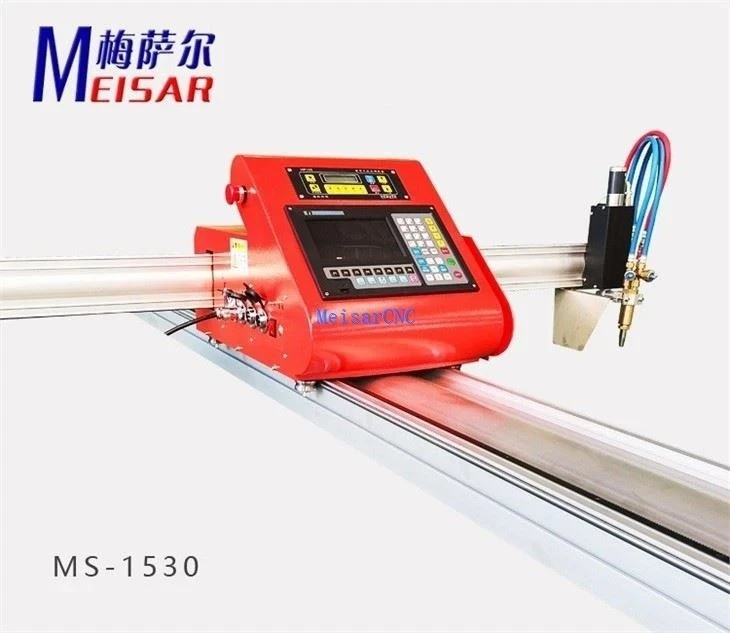
Product Identification & Core Specifications
The system eliminates manual layout, template tracing, and secondary grinding by combining direct CAD/CAM file import with automatic material positioning.The system eliminates manual layout, template tracing, and secondary grinding by combining direct CAD/CAM file import with automatic material positioning.
|
Technical Parameter |
Standard Specification |
Heavy-Duty Configuration |
|
Max Profile Width / Height |
1000 mm x 500 mm (H-Beam) |
1500 mm x 800 mm (Customizable) |
|
Positioning Accuracy |
+/- 0.2 mm |
+/- 0.1 mm (Linear Axes) |
|
Cutting Process |
High-Definition Plasma / Oxy-Fuel |
Multi-axis 3D Plasma Bevel Cutting |
|
Bevel Angle Range |
-45 deg to +45 deg |
Continuous +/- 60 deg |
|
Drive System |
AC Servo Motors + Planetary Reducers |
Dual-side Rack & Pinion (Zero Backlash) |
|
Supported Formats |
DSTV, DXF, DWG |
DSTV (Direct import from TEKLA / Advance Steel) |
Product Selection Guide (How to Choose)
Configuration selection depends on throughput requirements and downstream welding standards:
For General Structural Fabrication (Buildings & Bridges):
• Configuration: Standard 4-axis CNC profile cutter with high-definition plasma.
• Application Focus: High-speed loading, automatic measurement of material camber/twist, and rapid piercing for plates and channels.
For Offshore & Heavy Industrial Manufacturing (Pressure Vessels & Rigs):
• Configuration: 6-axis or 8-axis 3D robotic profile cutting system.
• Application Focus: Complex weld preparation (V, Y, K bevels), heavy wall-thickness cutting, and seamless integration with structural detailing software.
Application Domain
Designed for production environments requiring strict dimensional compliance and weld-ready edge preparation:
Structural Steel Construction: Automatic coping, rat-holing, and end-cutting of columns and beams for high-rise buildings and infrastructure.
Shipbuilding & Marine Engineering: Processing stiffeners, bulb flats, and longitudinal framing components.
Energy & Infrastructure: Fabrication of wind tower flanges, transmission tower angles, and bridge truss segments.
Supplier Qualification & Manufacturing Standards
Factory production protocols focus on structural stability, mechanical precision, and safety compliance:
Machine Bed Structure:
Welded from heavy-wall structural steel tubing, stress-relieved via high-temperature annealing (600 deg C to 650 deg C), and machined on a large-scale CNC gantry milling center in a single setup to maintain bed parallelism.
Motion Kinematics:
Powered by industrial AC servo drives coupled with precision helical rack-and-pinion gearing, delivering smooth acceleration curves and eliminating mechanical vibration during high-speed contouring.
Quality Inspection Protocol:
Every machine undergoes laser interferometer calibration for positioning accuracy, ballbar testing for circular interpolation, and a continuous 72-hour dry-run load test prior to dispatch.
Compliance & Safety:
Electrical enclosures built to CE/UL standards using industrial-grade components (Schneider / Siemens). Safety light curtains and emergency stop loops integrated per ISO 13849-1.
Buyer Decision Criteria & ROI Analysis
Operational benchmarks for capital expenditure (CapEx) evaluation:
Labor Reduction: Replaces manual layout and template tracking with a one-touch CNC workflow, reducing cutting-floor labor by up to 60%.
Material Utilization: Integrated nesting software optimizes bar stock layout, minimizing scrap rates for expensive structural profiles.
Fit-Up Accuracy: Maintains edge preparation tolerances within +/- 0.5 mm, directly reducing subsequent welding prep and root-pass rework time.
Frequently Asked Questions
Q: Can the machine import DSTV files directly from TEKLA Structures?
A: Yes. The industrial CNC controller features native DSTV file import capability. Operators can load files generated in TEKLA, Advance Steel, or SDS/2 directly without manual reprogramming or intermediate post-processing.
Q: How does the system compensate for twisted or warped steel profiles?
A: The machine is equipped with a touch-sensing initial height control (IHC) probe combined with scanning routines. It maps the actual surface profile before cutting to adjust torch height dynamically, preventing collision and ensuring consistent cut quality despite mill tolerances.
Q: What power supply options are available for plasma cutting?
A: We integrate industrial plasma power sources (such as Hypertherm X-Definition or equivalent high-current systems) ranging from 130A to 400A, matched to carbon steel and stainless steel thickness requirements.
Q: What is the typical installation and commissioning timeframe?
A: Standard installation takes 5 to 7 working days, including mechanical leveling, electrical tie-in, software calibration, and operator training conducted by resident service engineers.
Request an Engineering Proposal & Quotation
To receive an exact technical specification agreement and formal quotation, please provide your application parameters:
Profile Types & Sizes: (e.g., H-Beam up to HEB 600, Channel up to UNC 300)
Material Grades & Max Thickness: (e.g., ASTM A992, Q355B up to 50 mm)
Required Cutting Process: (High-Definition Plasma vs. Oxy-fuel)
Target Software Workflow: (TEKLA / AutoCAD / SolidWorks integration)
[Submit Technical Specifications for Fast Quotation] (Direct RFQ Form)
Hot Tags: cnc channel steel cutting machine, China cnc channel steel cutting machine manufacturers, suppliers, factory