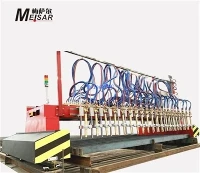
Heavy-Duty CNC Steel Pipe Cutting & Beveling Machine
Multi-Axis Thermal & Mechanical Profiling for Structural & Process Piping
Process large-diameter carbon steel, stainless steel, and alloy pipes in a single setup. Integrates automated loading, CNC 3D profiling, and precision bevel cutting to replace manual thermal cutting and grinding operations.
Engineering Specifications
|
Feature / Metric |
Specification Range |
Technical Detail |
|
Pipe Diameter (OD) |
50 mm - 1500 mm (2" - 60") |
Multi-range Chuck Options |
|
Wall Thickness |
3 mm - 60 mm (Flame) / Up to 25 mm (Plasma) |
Hypertherm / Kjellberg Plasma compatible |
|
Pipe Length |
6,000 mm - 12,000 mm standard |
Extendable modular bed options (Fits standard open-top shipping containers) |
|
Control Axes |
4-Axis, 5-Axis, or 8-Axis |
Yaskawa / Siemens Servo Motors |
|
Bevel Types |
V, X, Y, K, J-Prep |
+/- 45 degrees Torch Tilting Angle |
|
Positioning Accuracy |
+/- 0.2 mm per meter |
High-precision rack & pinion drive |
|
Max Pipe Weight |
Up to 10,000 kg |
Hydraulic self-centering support rollers |
|
Software Interface |
FastPIPE, MicroStation, Tekla, AutoCAD |
Direct DSTV / STEP file import |
Application & Joint Profiling Capabilities
This equipment handles complex 3D pipe end cuts and branch intersections without manual layout or post-process edge grinding.
Branch-to-Header Connections:
Saddle cuts, offset intersections, and multi-pipe branch nodes.
Structural Steel Fabrication:
K, Y, and T joints for offshore jacket legs, crane booms, and structural trusses.
Pressure Vessel & Piping Spools:
Straight beveling, J-prep bevels, and eccentric nozzle holes.
Mitre Cuts:
Multi-segment pipe elbows and bend profiling.
Core Component Quality & Build Standards
Machine Bed: Stress-relieved, welded steel frame annealed at 600 degrees C to prevent structural deformation over extended continuous operation.
Drive System: Precision helical rack and double-drive servomotors eliminating backlash during directional changes on thick-walled pipe profiles.
Torch Height Control (THC): Arc voltage THC with fast response loop (< 10 ms) compensates for ovality and straightness deviations in raw pipe stock.
Clamping Mechanism: Pneumatic or hydraulic 4-jaw Chuck featuring hardened steel grip jaws to prevent pipe slippage under high rotational torque.
Machine Selection Matrix
Choose the configuration matching your production parameters:
4-Axis Configuration: Best suited for straight cutting, basic beveling, and simple 90-degree saddle cuts on medium-wall piping.
5-Axis Configuration: Optimized for complex branch cuts, variable-angle V/X bevels, and structural pipe intersections.
8-Axis Configuration: Required for heavy structural steel profiling, thick-wall multi-pass bevels, automated pipe rotation, and inline hole cutting.
Plasma vs. Oxy-Fuel: Select Plasma for speed on stainless/carbon steel below 25 mm wall thickness; select Oxy-Fuel for carbon steel wall thickness exceeding 25 mm (up to 60 mm).
Factory Testing & Verification Standards
Every unit undergoes rigorous Factory Acceptance Testing (FAT) before shipment:
Laser Interferometer Testing: Axis positioning and repeatability verified over the full bed length using Renishaw laser alignment systems.
Bevel Geometry Audit: Bevel angle accuracy (+/- 0.5 degrees) measured via optical digital gauges across 360-degree pipe rotation.
Runout & Concentricity Check: Radial chuck runout held strictly within <= 0.15 mm.
Full Structural Test Cut: Test cuts performed on customer-specified pipe materials with DSTV file verification prior to dispatch.
Compliance Certifications: CE Marked (Directive 2006/42/EC), ISO 9001:2015 manufacturing facility, UL-listed electrical panels (optional for US market).
Frequently Asked Questions
Q: How does the machine compensate for out-of-round or bowed pipes?
A: The machine uses dynamic mechanical surface tracking combined with high-speed Arc Voltage Torch Height Control (THC). The tracking assembly maintains a constant distance between the torch tip and the pipe surface, taking real-time measurements to adjust the Z-axis instantly during rotation.
Q: Can the nesting software import 3D models directly from Tekla or AutoCAD?
A: Yes. The control software natively imports DSTV, STEP, and IGES file formats generated by Tekla Structures, AutoCAD, or Tribon. The software automatically extracts pipe dimensions, bevel angles, and intersection geometry without manual reprogramming.
Q: What is the typical edge roughness on a plasma-bevelled steel pipe?
A: Using a high-definition plasma power source (e.g., Hypertherm XPR series), ISO 9013 Range 3 or Range 4 surface finish standards are routinely achieved (Ra 12.5 - 25 micrometers). This surface quality allows direct robotic or manual welding without secondary grinding.
Q: What are the power and utility supply requirements?
A: Standard installations require a 380V/480V 3-phase, 50/60 Hz power supply. Compressed air requirements for plasma operation demand dry, oil-free air at 6.9 bar (100 psi) with an inline air dryer system.
Q: How is post-sales technical service handled for overseas installations?
A: We provide complete machine documentation, I/O mapping, wiring schematics, and remote diagnostic access via encrypted VPN controllers. On-site commissioning and operator training are conducted by factory-certified regional technicians or our dedicated international field engineering team.
Request An Engineering Review & Cutting Estimate
Submit your pipe outer diameter, wall thickness, bevel requirements, and sample CAD drawings (.DSTV or .STEP). Our technical team will generate a cycle-time analysis, container shipping layout, and machine specification quote within 24 business hours.
Hot Tags: cnc steel pipe cutting and beveling machine, China cnc steel pipe cutting and beveling machine manufacturers, suppliers, factory